Ingredient Handling Equipment
Simple installations to complete system design and integration, we help move bulk dry solids, powders, and occasionally slurries efficiently. Whether food, nutra, pharma, or industrial, we select the best-fitting equipment from the market instead of trying to fit our equipment to your product. Below you’ll find a far-from exhaustive list of popular equipment we distribute. If we seem like a fit but you don’t see the exact piece you’re looking for, fill out the form below; we can improve nearly any dry system.
Hand-Picked Equipment, cohesive systems
For dry bulk ingredients
Whether manufactured in-house or selected from the market, ABM identifies the best solution for your application. ABM engineers nail down minimum requirements, match existing options, make modifications if needed, and integrate the equipment into complete lines.
Our team has helped many hundreds of food, pharma, nutra, pet food, chemical, and industrial processors store, move, and feed dry ingredients efficiently.
Automate:
Equipment
Handling Equipment Categories
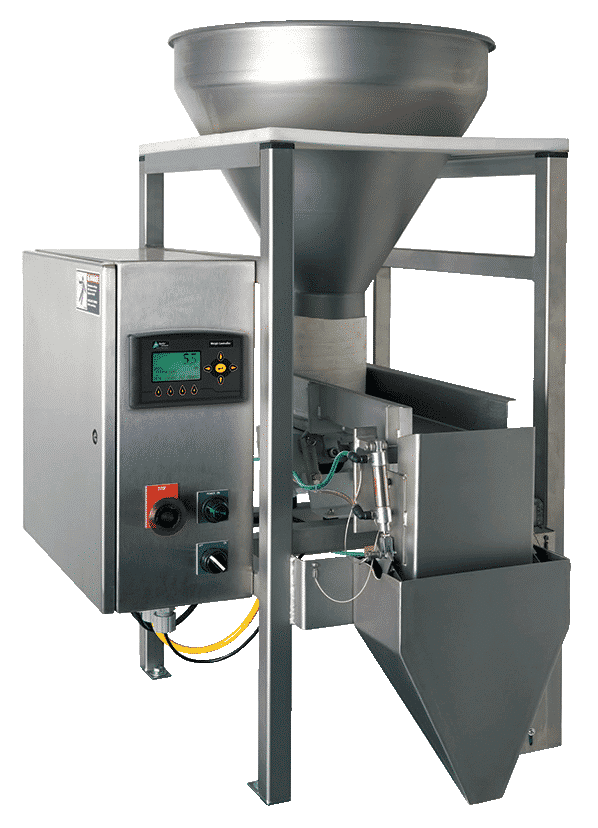
Vibratory Feeders
We offer several models in each of the divisions below to accurately dispense product in the needed increments whether grams or hundreds of pounds. Industrial to 3-A Dairy and washdown, we can integrate any feeder with conveyors, other equipment, and software.
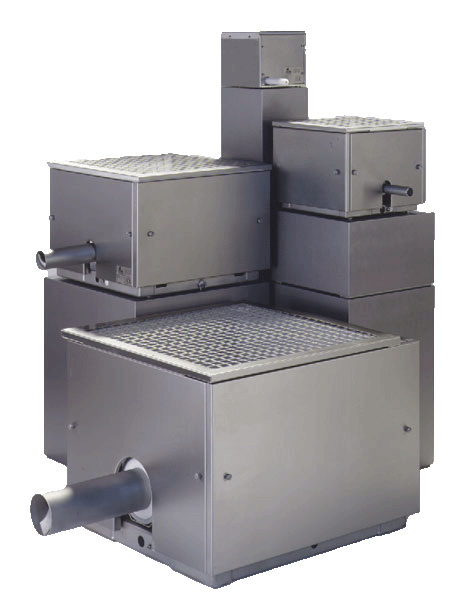
Screw Feeders
Whether you're handling powders, granules, chips, or other bulk solids, screw feeders give you the flexibility and control you need for accurate metering and consistent material flow. With over 50,000 units in use worldwide and a wide range of models and configurations, these screw feeders are designed to fit nearly any environment or application.
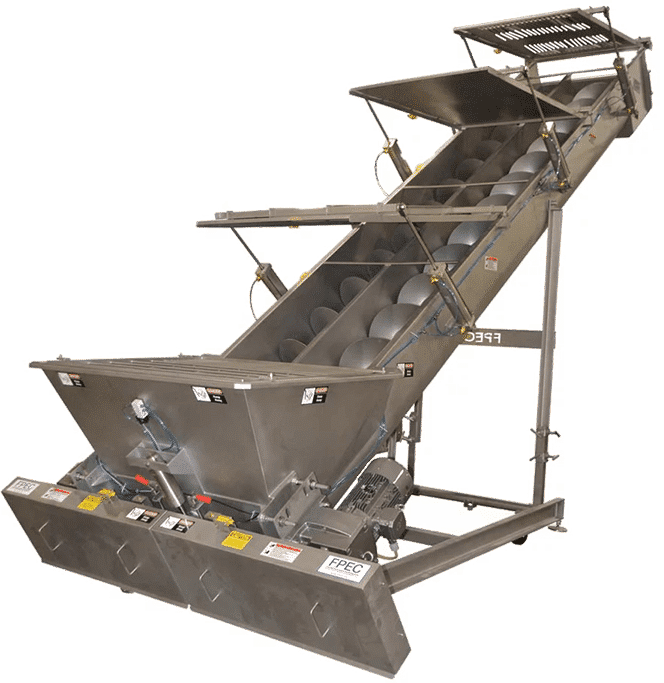
Screw Conveyors
Screw conveyors are one of the oldest conveying methods known to man and still the ideal method for many applications. Though screw conveyors and augers are technically synonymous (any conveyance method driven by rotating threads) the processing industry typically reserves the term “screw conveyor” for larger executions, and augers for enclosed, tubular conveyors. For precise metering using screws, see screw feeders.
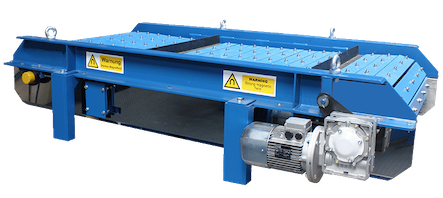
Magnetic Conveyors
Home » Ingredient Handling Equipment Ingredient Handling Equipment Magnetic conveyors use magnetic fields to transport and manipulate bulk materials either by moving a magnetic belt or gripping ferrous materials through the belt for sorting. We use them in recycling applications to separate metal from carboard and plastic as well as manufacturing applications for pulling metal […]

Vibratory Conveyors
Vibratory conveyors vibrate a sloped metal plate to make loose solids flow. We use them for many products that need gentle, short-distance conveyance, most commonly pharmaceuticals and ingredients. We integrate the flat, open designs that most people are used to seeing as well as tubular 3A models.

Spiral Conveyors
ABM supplies spiral conveyors to move units of product vertically where floor space is limited, space is needed for accumulation, or the product needs more dwell time on the best for cooling. We provides spiral conveyors from a number of different OEMs depending on the best combination of quality, cost, and features for your application. From selection and drawings to customization and integration, ABM handles your project from conception to maintenance.

Tubular Drag Conveying Systems
ABM supplies tubular drag conveyors for most non-abraisive, free-flowing products including powders, pellets, and granules. Capacities can vary depending on the configuration and product, but as a reference, tubular drag conveyors reach capacity with milled grain at 2,000 ft. through 24 elbows and conveying at a rate of about 300 pounds per hour.
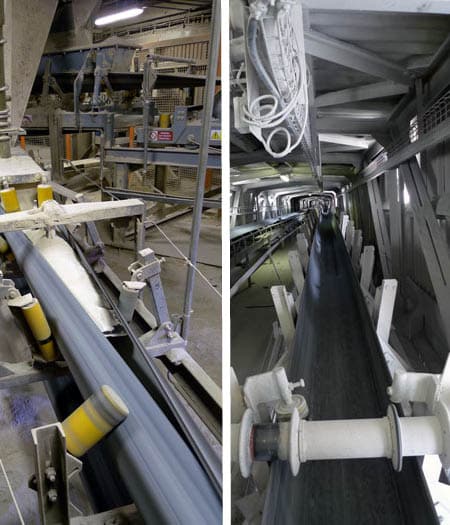
Tube Belt & U-Belt Conveyors
Home » Ingredient Handling EquipmentIngredient Handling Equipment We use tube and u-belt conveyors most commonly in industrial settings to transport bulk materials. They are open along the run where product is being loaded, then are closed by devices and rollers. However, there are some key differences between the two types of conveyors that can affect […]
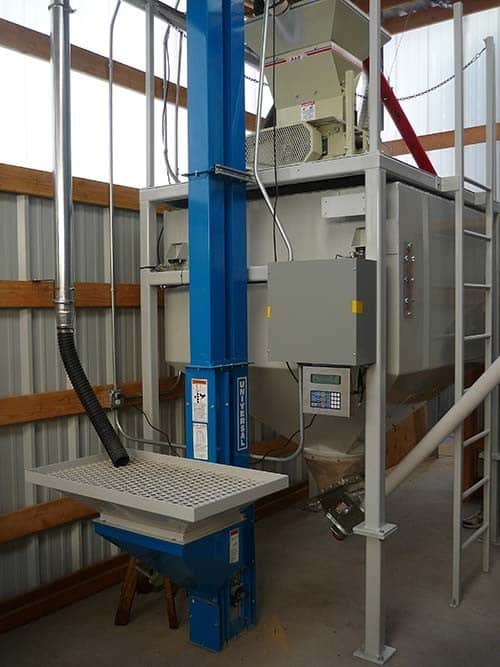
Bucket Elevators
ABM uses bucket elevators are to lift bulk dry ingredients within a small footprint. They consist of a series of buckets attached to a belt or chain, which runs over a pulley or sprocket at the top and bottom of the unit. The buckets scoop up material at the bottom and then lift it to a higher point, where the ingredient is discharged.
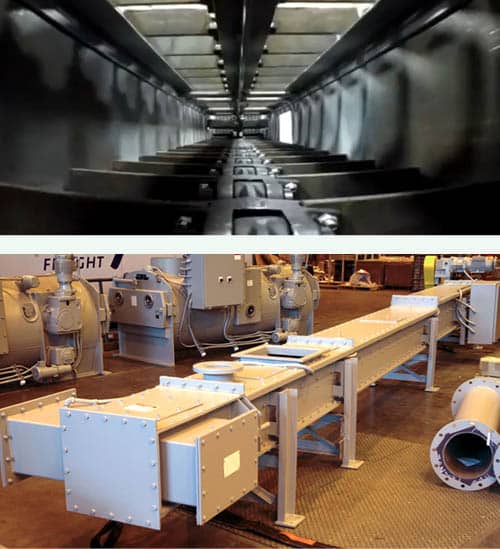
Chain Conveyors
Chain conveyors, not to be confused with chain-driven belt conveyors, or tubular drag, use gear-driven chains to move materials along a conveyor path. ABM provides different configurations to move large, heavy objects such as boxes and pallets, or varous kinds of loose material with specialized paddles.
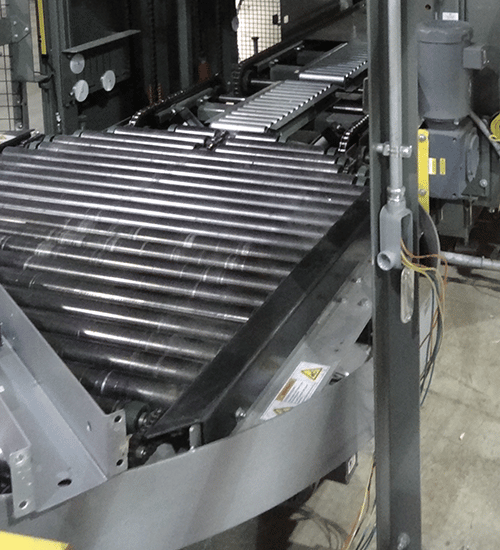
Roller Conveyors
ABM Equipment provides both powered and gravity roller conveyors for boxes and large packaged goods in manufacturing, warehousing, and distribution applications. We use powered roller conveyors for controlling product spacing, controlling speed of incoming product, and conveying different products independently on the same conveyor.
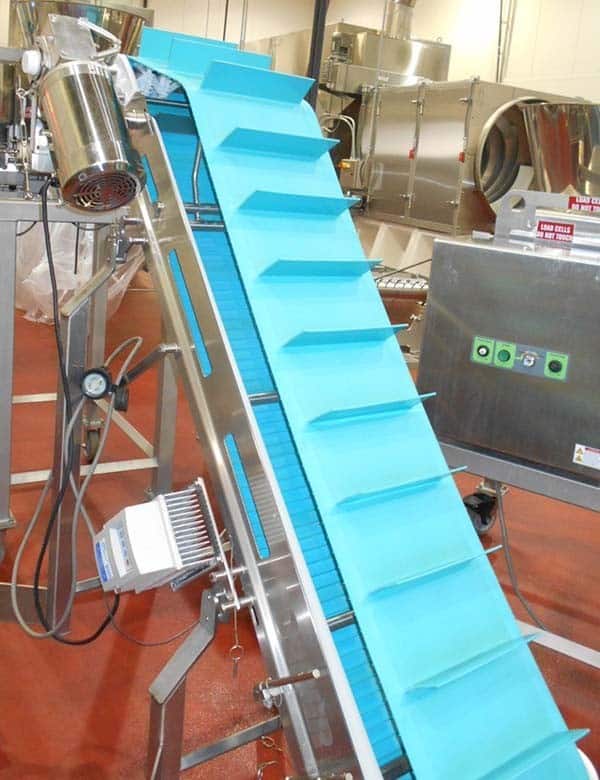
Cleated Belt Conveyors
Cleated belt conveyors are standard conveyors with raised edges (cleats) to keep product in place and prevent it from sliding or falling off the belt as it moves. This allows greater capacity and conveyance up slopes. The cleats can be made of various materials such as plastic, rubber, or metal, and can be arranged in different patterns depending on the type of material being conveyed and the needs of the application.

Silo Sales
Silos for every application from aggregates to agriculture and food ingredients, with options for all environments, and with the related equipment for every application. We handle your whole project from engineering and fabrication to integration and controls.
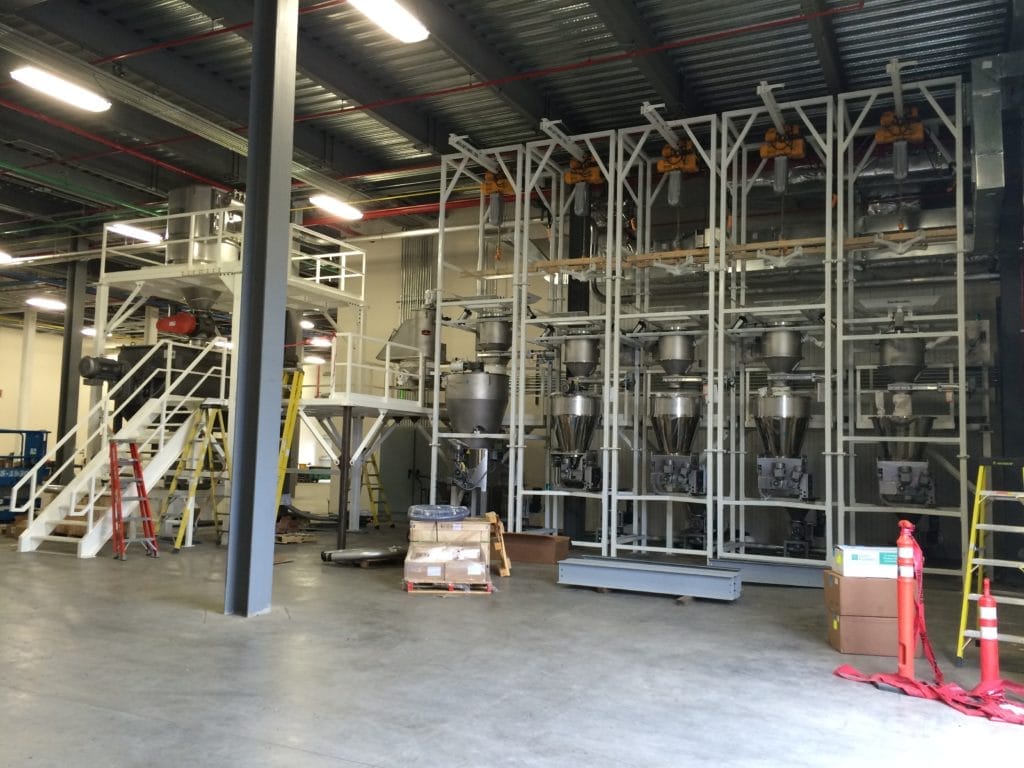
Bulk Bag Unloaders
We provide bulk bag unloaders (BBUs) for food, nutraceutical, pharmaceutical, and chemical manufacturing systems. There are many configurations available on the market, so whether we source or build them will depend on your needs. The benefits of moving to BBUs (assuming your ingredient demand warrants them) are listed below.
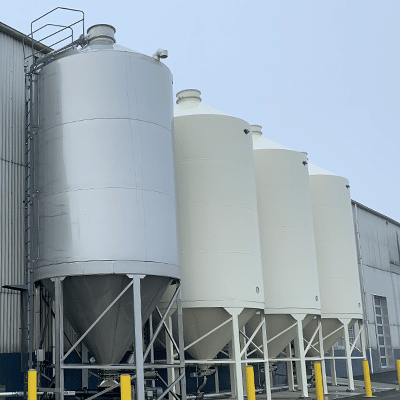
Silos
ABM Equipment provides silo sales and servicefor food, chemical, and nutraceutical applications. ABM Equipment handles process engineering, mechanical engineering, integration, and service for silos, as well as our own custom leak-proof gates. We will design your system, help navigate zoning and seismic requirements, and find creative ways to satisfy or avoid other municiple requirements.
Work Bins
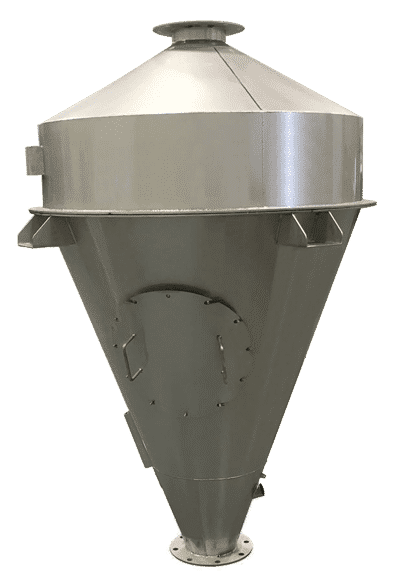
ABM fabricates and sources work bins of all types, from totes on wheels to product staging in continuous processes, in all metal materials from carbon and stainless to aluminum. We handle install, integration, and service on all intake and discharge conveyance as well as surrounding equipment.

Level Indicators
ABM sources the best combination of models, features, accuracy, reliability, and price for you application from all suppliers on the market. BinMaster has a product guide which is useful for comparing methods for level detection, and we've provided a summary of the common options below. The recommended supplier for your application, however, will depend on your situation. Browse below or skip the work and send us a message to find your viable options.
Over 50 years of experience
ABM has spent decades delivering custom-engineered solutions for dry bulk ingredients and